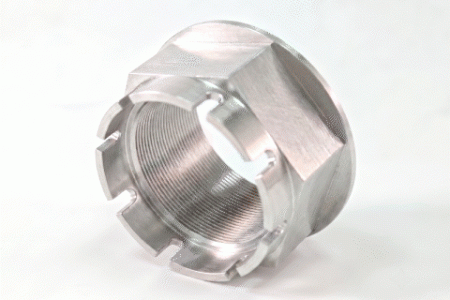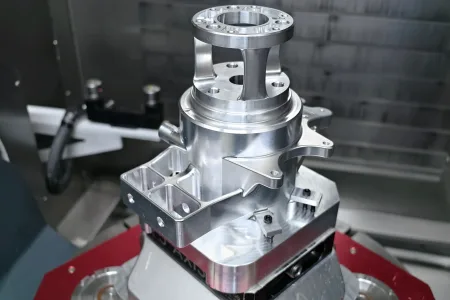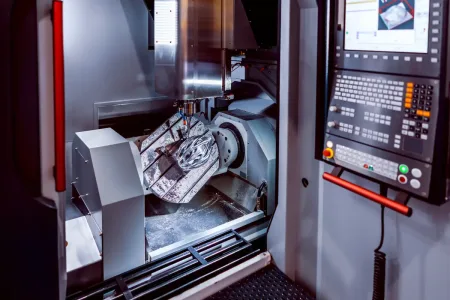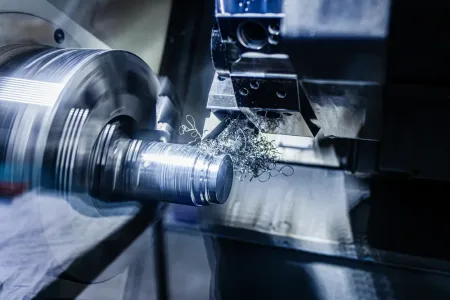
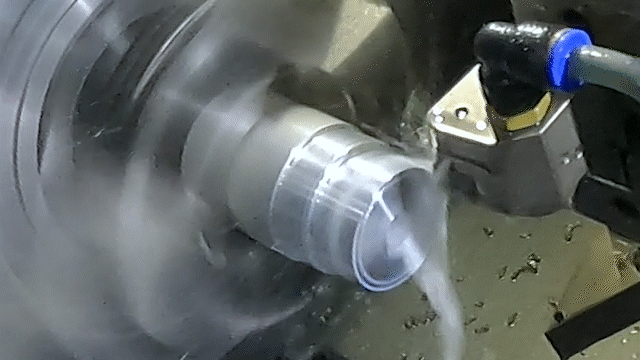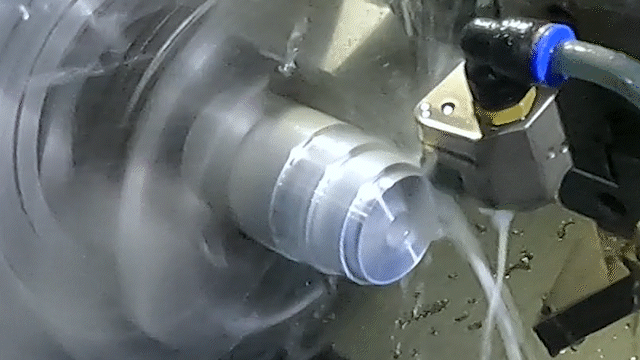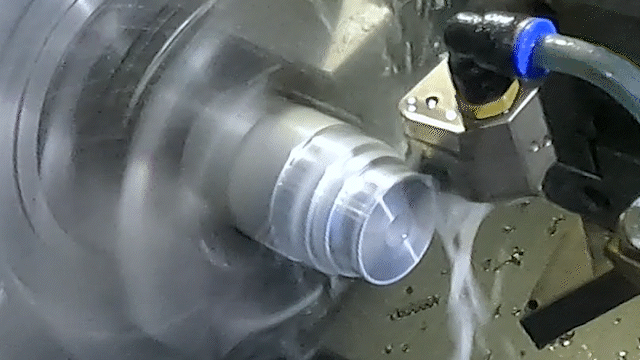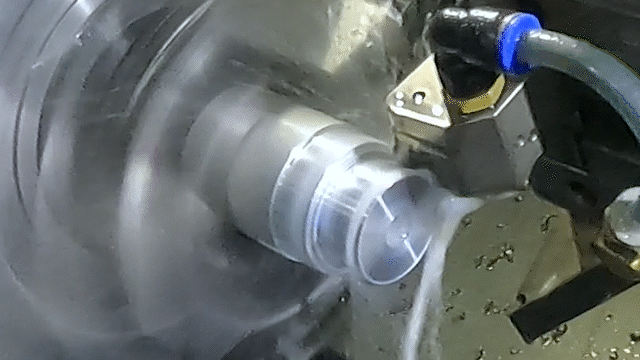
Modern multi-axis CNC turning centers combine the high precision and fine surface finishes of conventional lathes with the versatility of milling machines. Because live tooling moves independently of the spindle, turning centers produce many complex geometries in a single setup, saving valuable time and money while preserving tight tolerances.
What is a traditional lathe?
A traditional lathe rotates a workpiece horizontally while it’s held firmly on at least one end. Cutting and shaping tools are applied to the workpiece as it spins, meaning this basic process is ideal for making round and cylindrical parts.
What is a manual lathe?
With a manual lathe, the operation of the cutting tool is controlled by mechanical inputs from a skilled technician. While still in use today for some specialized work, manual lathes are much too slow and imprecise for modern high-speed parts manufacturing. They also pose considerable danger to the operator if they stand too close to the moving spindle.
What is a CNC lathe?
In a CNC lathe, digital software regulates the rotation of the workpiece and the toolpath of the cutting tool. This greatly increases speed, accuracy, and repeatability, while keeping the technican safely out of harm’s way.
Although they’re fast and reliable for production manufacturing, conventional CNC lathes are still limited in the number of operations they can perform. Some features require the part be dismounted and located on a different machine.
What is a multi-axis CNC turning center?
Unlike a conventional lathe, a multi-axis CNC turning center has a separate spindle with its own set of live tools. This spindle moves independently of the central axis, creating new machining possibilities. Each additional axis of motion translates to greater versatility and more efficiency.
This is possible because the workpiece is kept stationary while the live tooling performs milling operations. Milling makes flat, prismatic shapes, contours, slots, and other features that are impossible to produce on a standard lathe.
What are the benefits of multi-axis motion for precision CNC turning?
Product developers turn to precision CNC turning services because of the many benefits they provide. These include:
- Fewer setups and remounting
- Tighter tolerances
- More complex part features
- Shorter production lead times
- Decreased production costs.
Explore the Possibilities of Multi-Axis CNC Turning.
Learn how multi-axis CNC turning services can help you save time and money while getting better parts faster.
What are the major multi-Axis CNC turning operations?
Now that we understand the basics of how CNC turning machines work, let’s examine the different operations they can perform.
Drilling
One of the most basic of all machining operations is drilling. Drilling makes a hole in the workpiece using a helical drill bit. On a lathe this means the workpiece turns while the stationary bit is pressed into it at a controlled rate. Helical flutes along the shank of the bit help to draw waste material out and away.
Drilling can make thru-holes, stepped or blind holes, and can also be followed with secondary operations like boring, reaming, or tapping.
Boring
Drilling removes a lot of material quickly, but the wall surface can be rough. That’s why boring is used to further refine the hole size and its shape (concentricity).
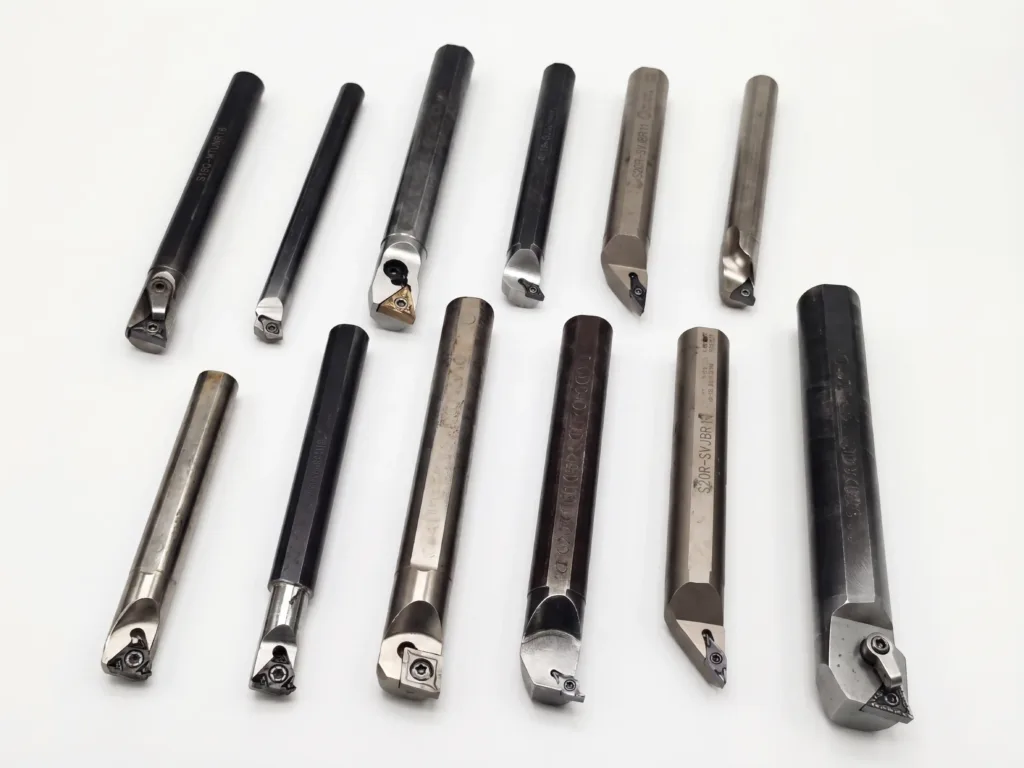
Boring often employs a single bit mounted on a bar. It’s more accurate than drilling and is widely used in automotive, engineering, and industrial applications. You’ll find boring used to make precision gun barrels, engine block cylinders, and clearance fit holes for mounting pins, bearings, and bushings.
Reaming
Similar to boring, reaming is used to slightly enlarge a pre-existing hole to achieve a final dimension and surface finish. Unlike a bore which has a single cutting bit, a reamer has a shank with helical cutting faces that remove micro-amounts of material.
As with boring, tolerances of +/- 2 m or better can be achieved. Tolerances tighter than this become increasingly difficult in all hole-making operations, because the workpiece tends to warp in response to the heat and pressure of the cutting tool. Also, long boring tools have a tendency to vibrate at the tip which causes tolerance drift.
Reaming is especially useful for making holes into which will be inserted press-fit dowel pins. These are often found on split engine cases and other industrial assemblies that need to be periodically opened and closed for maintenance.
Tapping and Threading
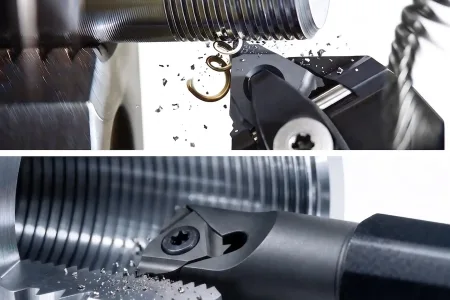
Once a hole is made via drilling, tapping can be used to form internal threads for screws and bolts. Tapping can be done on both through and blind holes but note that in a blind hole the tap won’t be able to reach all the way to the bottom.
Tapping produces internal threads, while “threading” refers to the external geometry on the shaft of the mating bolt or screw. Threading can be done with a CNC turning center, but high-speed production of screws and bolts usually calls for a dedicated screw-cutting lathe such as the classic Browne and Sharpe.
Turning
This is a broad category of machining operations performed on the workpiece to alter its external shape using various cutting and forming tools. The most common varieties are:
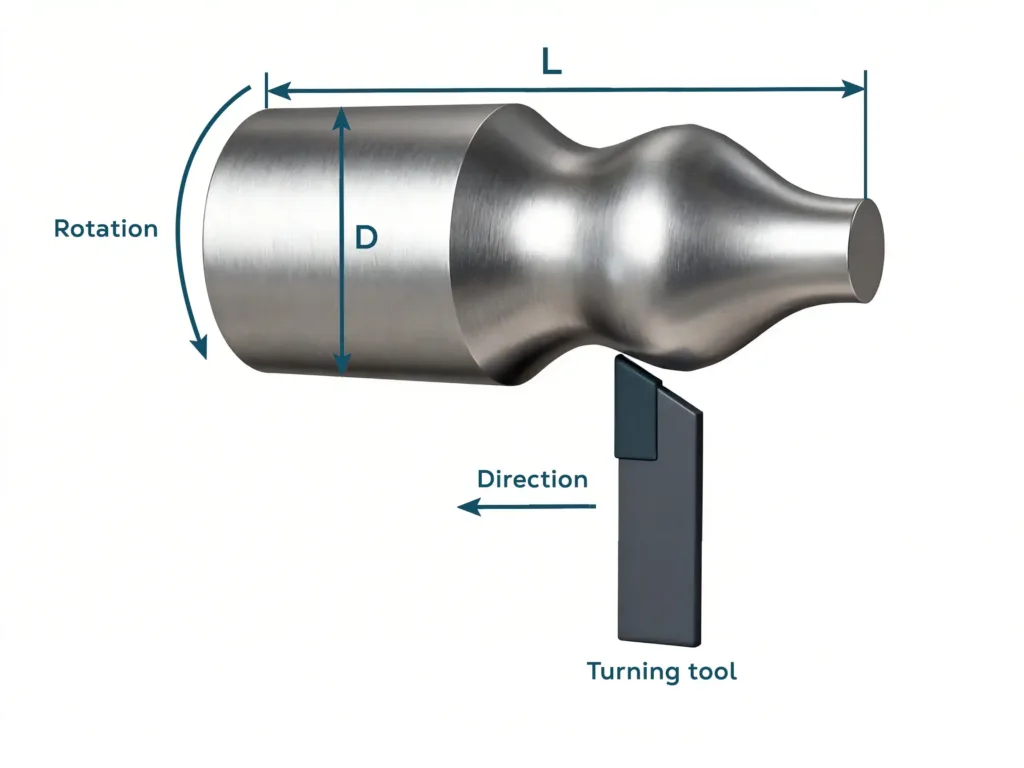
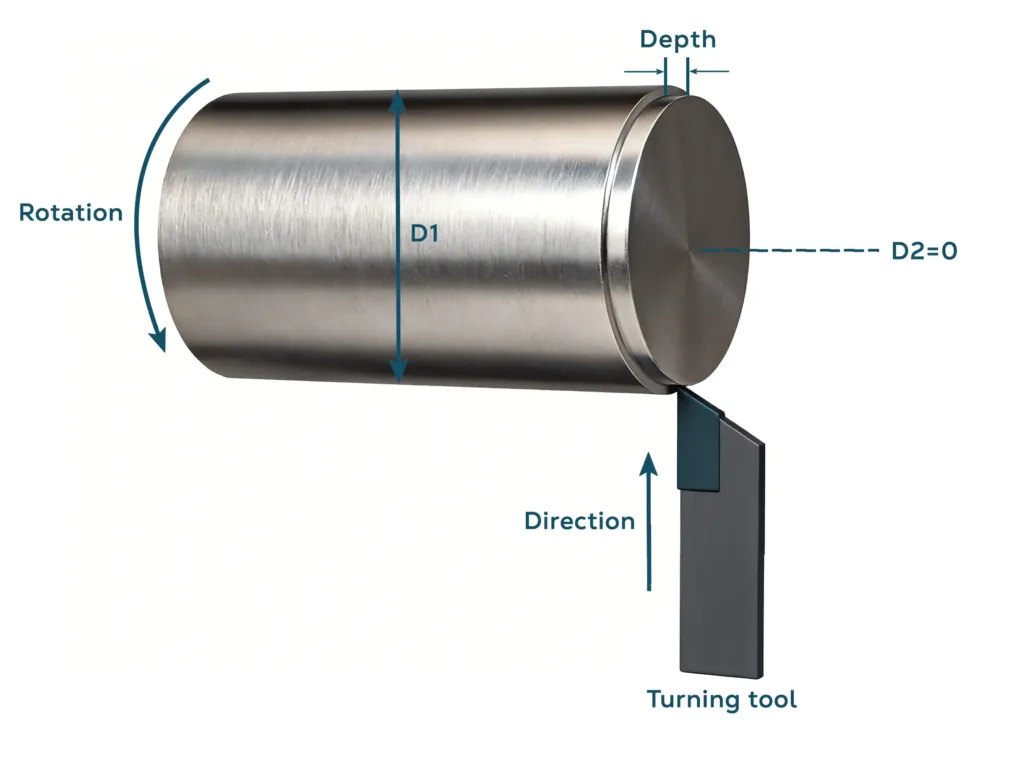
- Contour Turning. For making symmetrical but non-cylindrical shapes, contour turning varies in both diameter and cutting angles along its axial length. This creates more complex and rounded profiles than a simple taper.
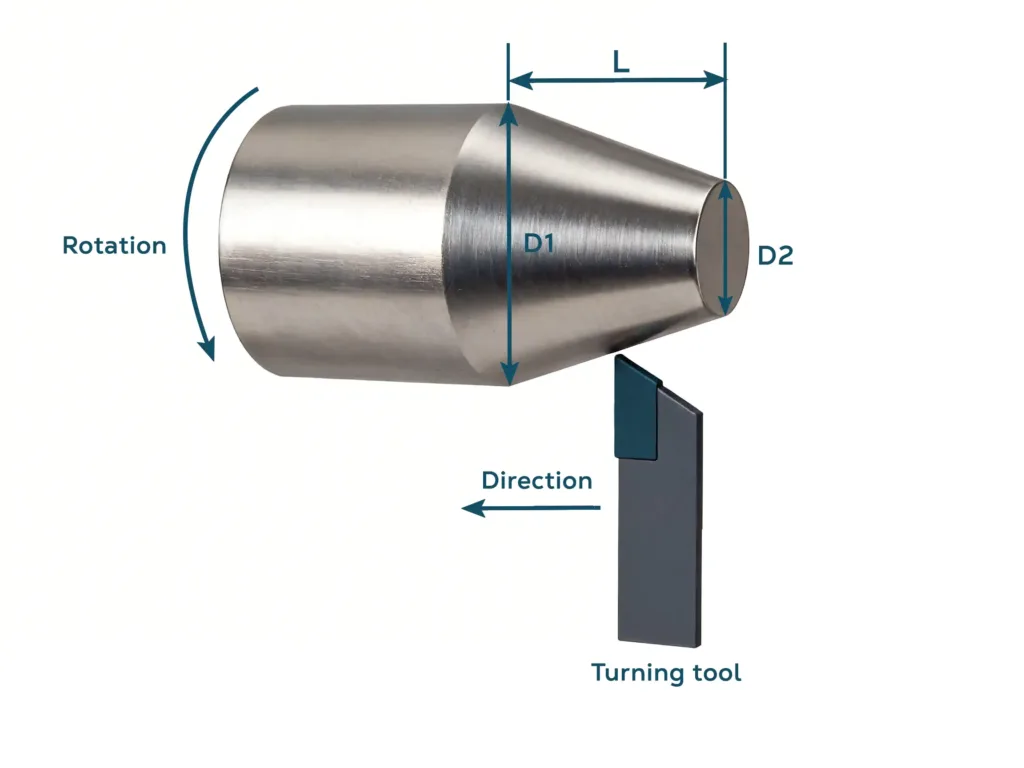
- Taper Turning. Taper turning applies a relatively simple conical or pointed shape to the workpiece, which varies in diameter along a single unchanging angle relative to the central axis. A chamfer is a form of taper turning applied to the end of the part to create a softer transition between two angled faces.
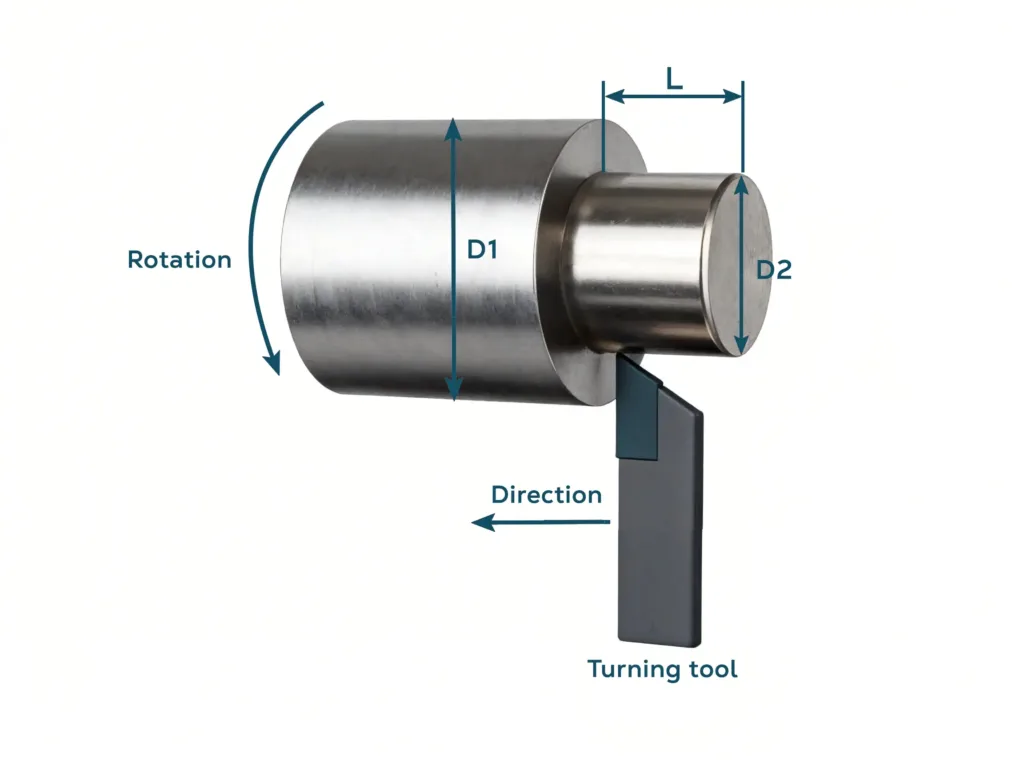
- Shoulder Here the cutting tool is used to impart a diameter on one section of the workpiece where it meets another diameter at right angles.
- A cutting tool is used to make a flat face on the end of the workpiece, at precise right angles to the axis of rotation. This is often done to make a reference position for measuring other dimensions on the part.
Knurling
Knurling relies on a specially formed tool with a diamond or cross-hatched pattern which is pressed against the workpiece to transfer the pattern’s design.
Knurling is sometimes done for cosmetic reasons, but its main purpose is to improve the gripping surface on handles and shafts.
Grooving
A special grooving tool is used to machine a radial slot or groove in the workpiece with a controlled width and depth. Such grooves can hold snap fittings or provide clearance for other components.
Parting
It’s sometimes necessary to remove the finished or semi-finished part from the remaining bar stock which is still mounted in the holding chuck. A thin parting tool cuts all the way to the centerline, after which the workpiece falls free into a basket or tray.
What milling operations can a CNC multi-axis turning center perform?
In addition to normal lathe turning operations, CNC turning centers incorporate live tooling and an independent spindle to perform traditional CNC milling operations, thereby greatly increasing their versatility. Adding an additional 3,4, or even 5 axes of travel then opens up many more pathways the machinist can use to make complex shapes that combine both turned and milled features.
When live tools are used on a workpiece that’s mounted in a chuck, the chuck is held stationary.
They can drill holes off-center to the main axis, create flat faces and prismatic forms, or contour complex shapes and undercuts – without ever needing to dismount the workpiece.
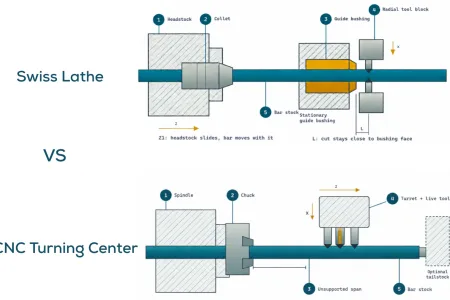
In addition, some turning centers, like precision Swiss-type lathes, can machine the back of a part as well – impossible to do in one setup with either a standard lathe or conventional mill. This is so helpful when creating complex fasteners and turned fittings that must maintain precise tolerances.
What types of material can be turned on a lathe?
CNC turning can work with many rigid metal and plastic substrates.
| Machinability | Material |
|---|---|
| Good | Aluminum, brass, magnesium, 174-PH, 303/304 stainless, P20, NAK80, most mild steels, all engineering resins |
| Medium | Bronze, tungsten copper, berrylium copper, tool steels |
| Poor | Titanium, superalloys |
These are just a few examples of the most common turned metal and plastic materials. Contact our engineers to discuss your particular needs in detail and we can recommend the best material to suit.
In all cases, the raw material must be rigid enough to withstand the cutting force of the tool without deforming. Carbon fiber and other composites are a poor choice because, although they are rigid, they tend to shatter and don’t form good cutting chips.
Materials differ in how easy they are to machine, mostly due to the presence of sulfur which helps the machining process. Superalloys and titanium require the use of very hard and sharp cutters and extreme care with speeds and feeds.
What precision tolerances can be achieved by CNC turning?
Multi-axis CNC turning centers can achieve 5 microns or better on a regular basis using standard materials and tools. For extremely tight tolerances, 0.5 microns is achievable, but this demands carefully controlled environmental conditions and superior equipment.
Typically, such a degree of accuracy is only required for the most demanding applications in aerospace, security, and scientific instruments. For most consumer applications 3~5 microns is more than acceptable.
What kind of surface finishes are possible with CNC turning?
Multi-axis CNC turning produces beautiful surface finishes. The value is measured in Ra. The lower the Ra value, the smoother and flatter the result.
One of the reasons the surface quality is so good with CNC turning is because the cutting tool stays in constant contact with the workpiece. Compare this to the periodic chipping away that’s done on a CNC mill.
Different raw materials produce different Ra values depending on their machinability and chemistry. Also note that not every project needs or wants to have a very smooth surface. Sometimes surface roughness is a desirable condition for the part’s application.
Let’s take as an example carbon steel 12L14, one of the most machinable mild steels. It can achieve a surface Ra of 0.4m, making it smooth enough to be used in bearings, rollers, shafts, and other CNC turned parts that must spin with low friction and high wear resistance.
What are examples of parts made using CNC turning centers?
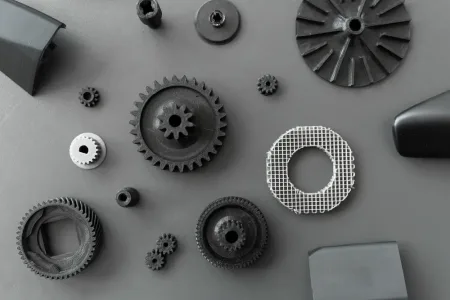
Here are just a few examples of the many types of components made with multi-axis CNC turning centers:
- Splined shafts
- Helical gears
- Rotors
- Screws, bolts, specialty fittings
- Axles and drivetrain components
- Actuator rods
- Pistons, cylinders and hydraulic components
- Bushings and rollers
Virtually any product with a central axis of rotation can be made via CNC turning.
What are the advantages of CNC turning centers for making complex parts and prototypes?
Equipment engineers continue to find new ways to improve the substantial advantages of these remarkable machines which offer:
- CNC Turning and CNC milling in one setup
- High tolerances
- Excellent surface finishes
- Complex geometries
- Material versatility
- Bar feeding for uninterrupted production
High speed digital manufacturing of bespoke rapid prototypes and production parts is greatly enhanced with the use of multi-axis CNC turning centers. That’s why Procision Manufacturing has invested in dozens of imported horizontal and vertical milling centers and high-precision Swiss-type lathes.